Manufacturing Steps How a bespoke disc spring is made
We thought we’d explain the manufacturing process, so that you can appreciate the lead times on any bespoke or custom disc spring order, and the high cost of manufacturing these items.
Our Quality Management System is tightly integrated into the manufacturing of our disc springs and related products, from end to end. The basic manufacturing steps are as follows.
Design Verification
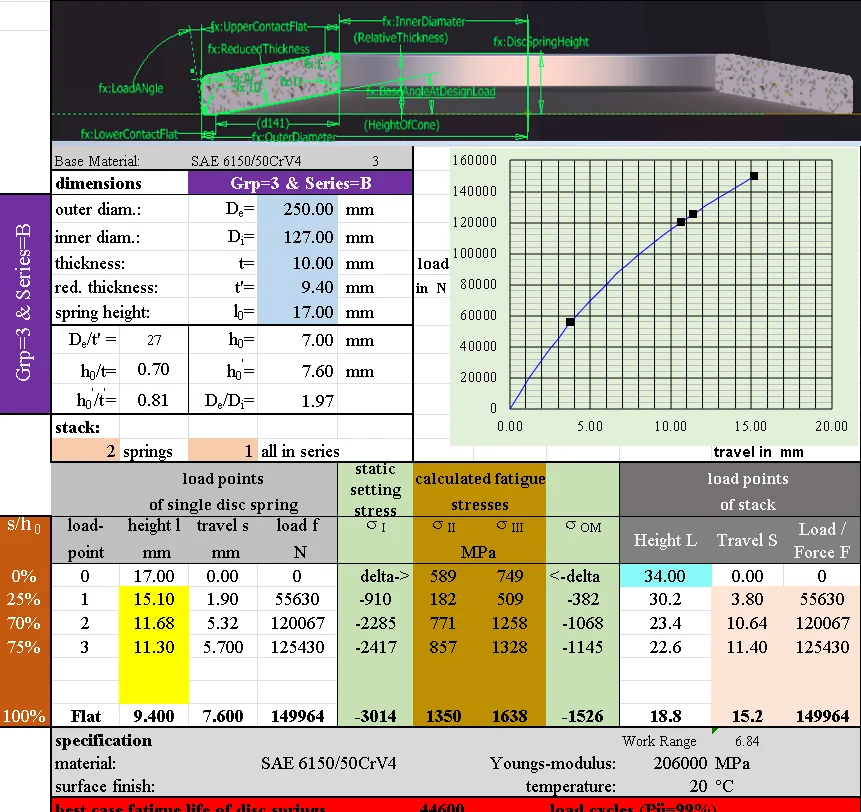
As part of our ISO 9001:2015 Quality Management System, we produce a disc spring design with all the properties you can expect from both the individual disc spring and the stack, in whatever configuration you will use it. Here’s an example. All of this information goes into the job card pack that accompanies the quality assurance pack through the manufacturing process. We have a page dedicated to design verification.
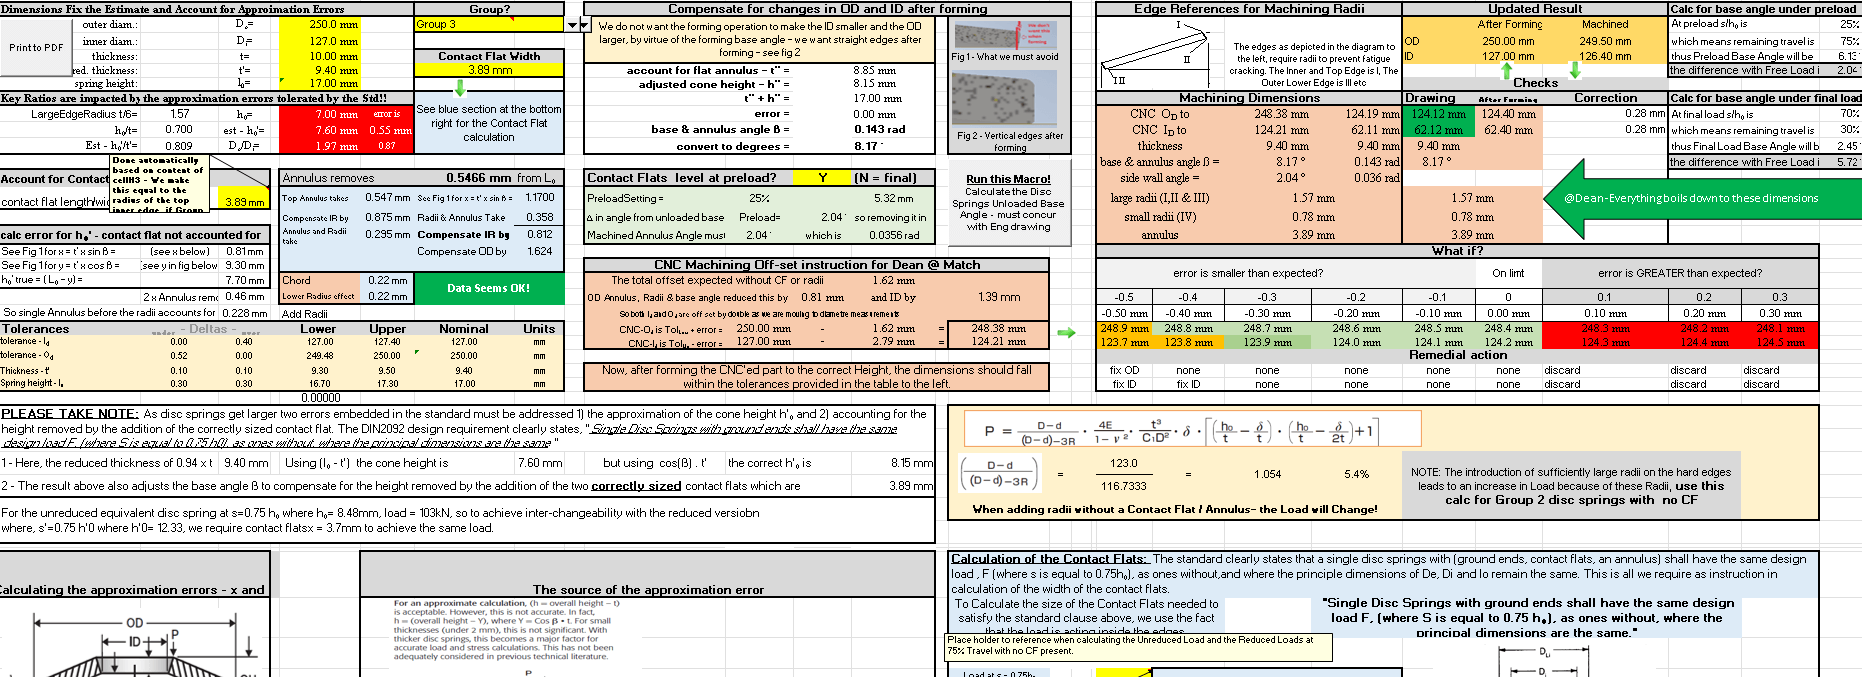
Our results may differ from those of most other manufacturers, because we use an updated method to calculate the contact surface (annulus) dimensions. This is extremely important for disc springs with De greater than 150 mm. Even more importantly, especially where disc springs are used in stacks, we account for friction in our stack designs.
Planning & Oversight
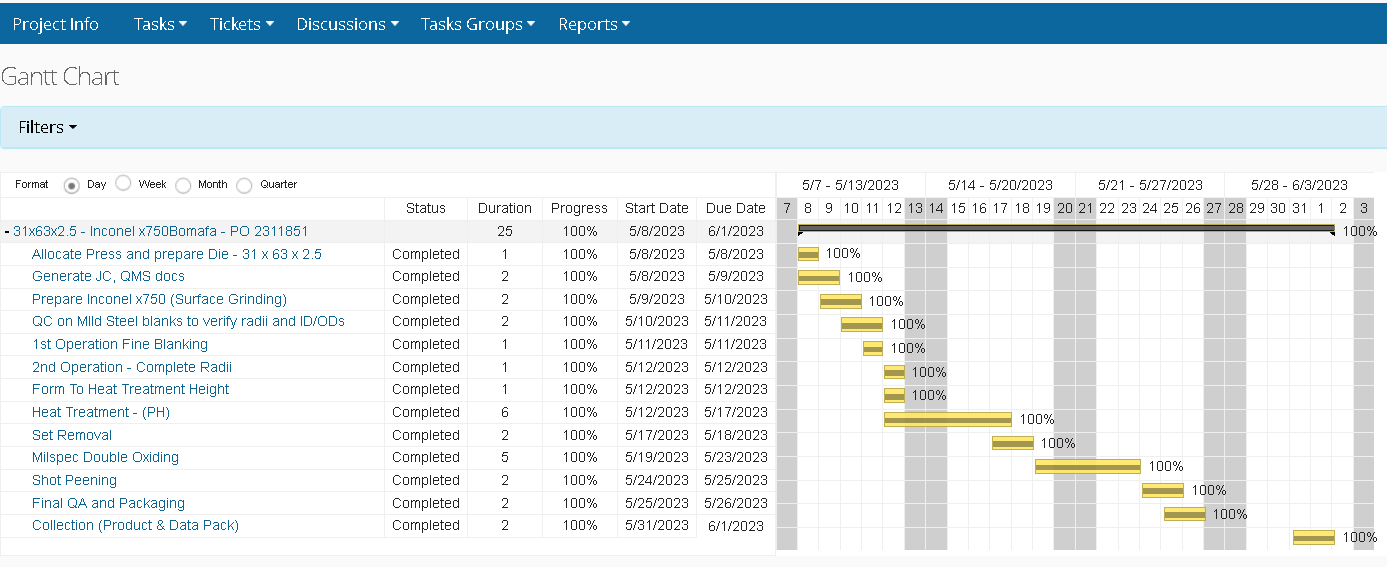
We often have to integrate our planning into large engineering projects. When we do, we give you a login to our online tracking tool.
There we present the project plan as a Gantt chart, and each deliverable has all the associated documentation or evidence attached to it. Our large engineering clients love this tool.
Materials Prep
With a few exceptions, nearly all available tables and data sets are calculated with a Young’s modulus E of 206 000 N/mm2 and Poisson’s ratio μ = 0.3. They are therefore only valid for disc springs made of the spring steels in DIN EN 16983, to DIN EN 10132-4 and DIN EN 10089 (for example C75S / SAE 1075 or 51CrV4). Other materials need a recalculation with the correct Young’s modulus.
The material arrives in plate form with material certificates. We order excess material so that any rework is not delayed by having to source material again. The material is first sandblasted to remove scale, and then surface ground to give a uniform thickness for the workshop processes.
The quality management plan, as set out in the online tracking tool, places the first client QA hold point here. This covers the material test certificates for chemical composition, Young’s modulus and material uniformity. The thickness tolerance across all the disc spring types in a project is ±0.1 mm, and it is applied to t′ for disc springs with contact surfaces.
Alternative materials
The vast majority of our orders are for disc springs working in non-corrosive environments at moderate temperatures. Where the environment demands it, we use an appropriate material, for example:
- where the operating temperature is high (above about 150 °C, the limit for 51CrV4), heat-resistant steels or, at the highest temperatures, Inconel X-750 or 718;
- where the environment is corrosive, stainless spring steels such as AISI 301 (1.4310) or 17-7 PH (1.4568);
- where a non-magnetic material is needed, copper-beryllium (CuBe2), tin bronze (CuSn8) or Inconel, since stainless spring steels become magnetic when cold worked.
For a review of the materials we use, see our materials page.
Blank profiling
This step is necessary for all precision CNC-machined Group 3 disc springs. We have the plates laser cut into blanks with Dprofile > De, which allows more efficient nesting and better yields. For large engineering projects with demanding timelines, we plan at least 5% extra blanks to mitigate the risk of rework or quality assurance failures. No engineering customer has ever faced penalties because of late delivery by us!
CNC Machining
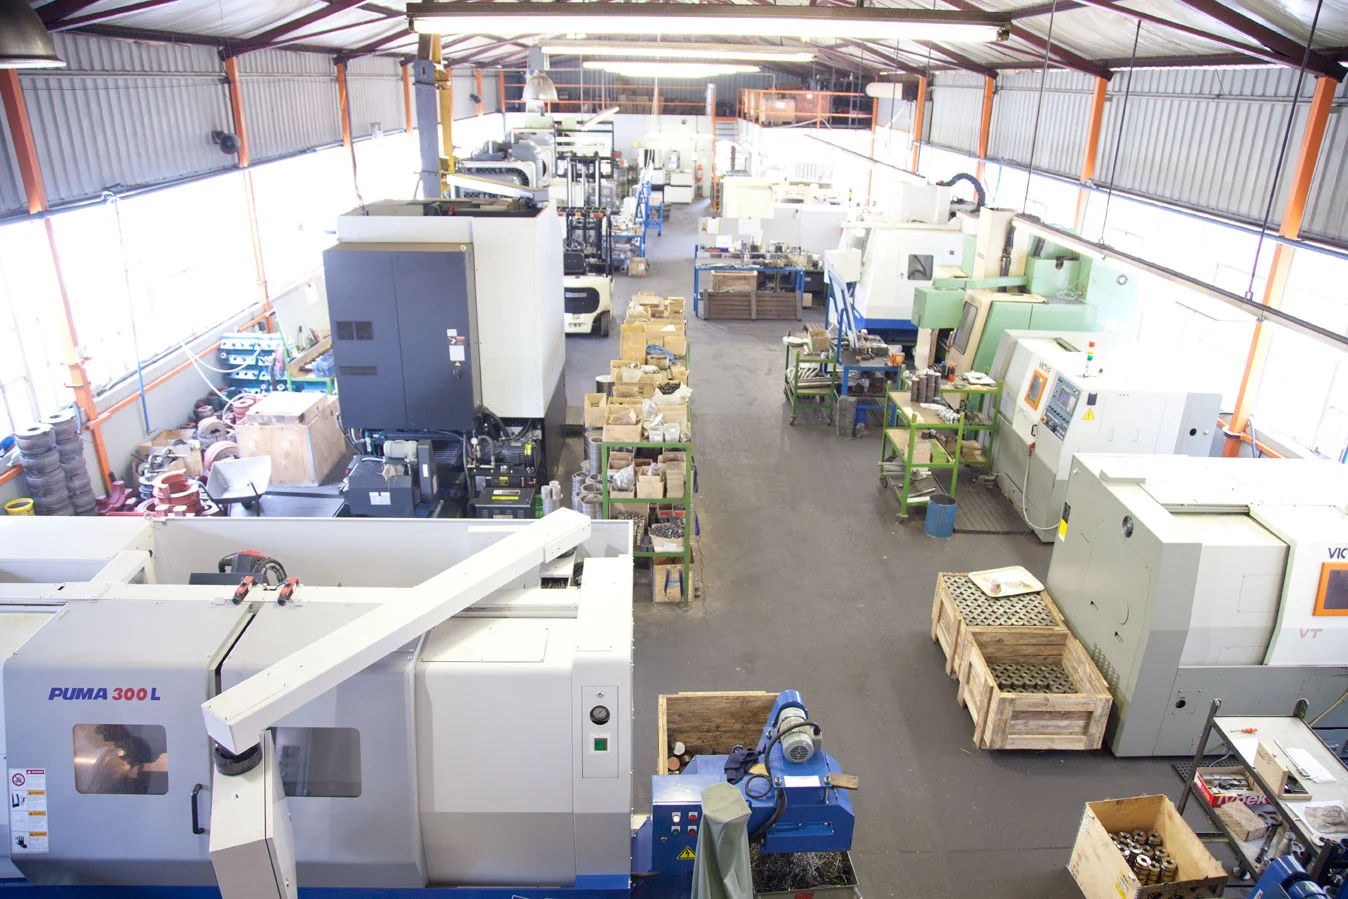
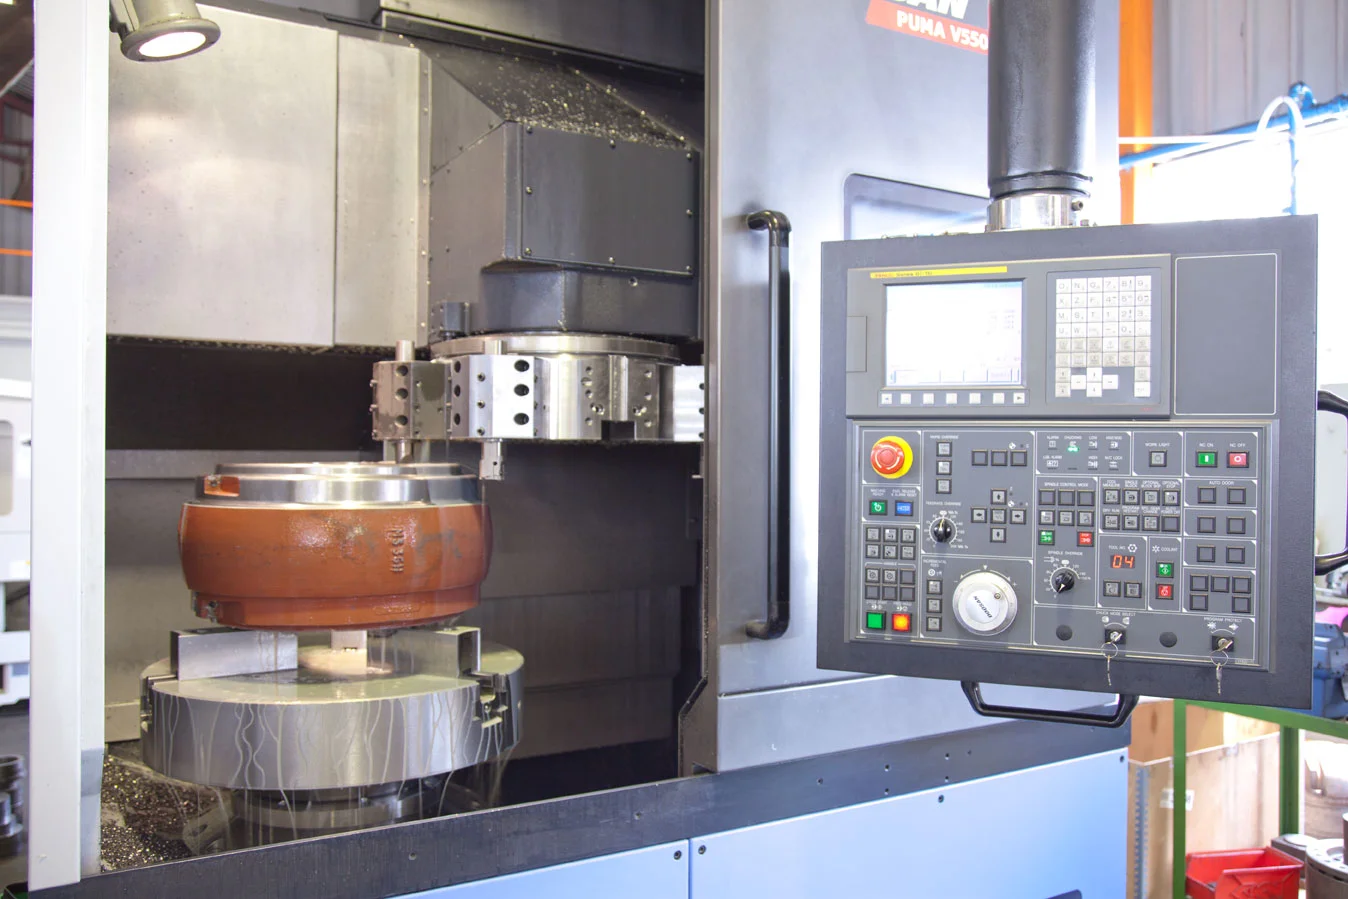
The detailed design of each disc spring’s contact surfaces is part of the data pack. This stage includes the preparatory surface grinding that ensures the thickness t′ is well within tolerance. The top and bottom load-bearing flats are machined at the specified final cone angle, so that they are level once forming is complete. All radii are added at this stage as well.
Forming
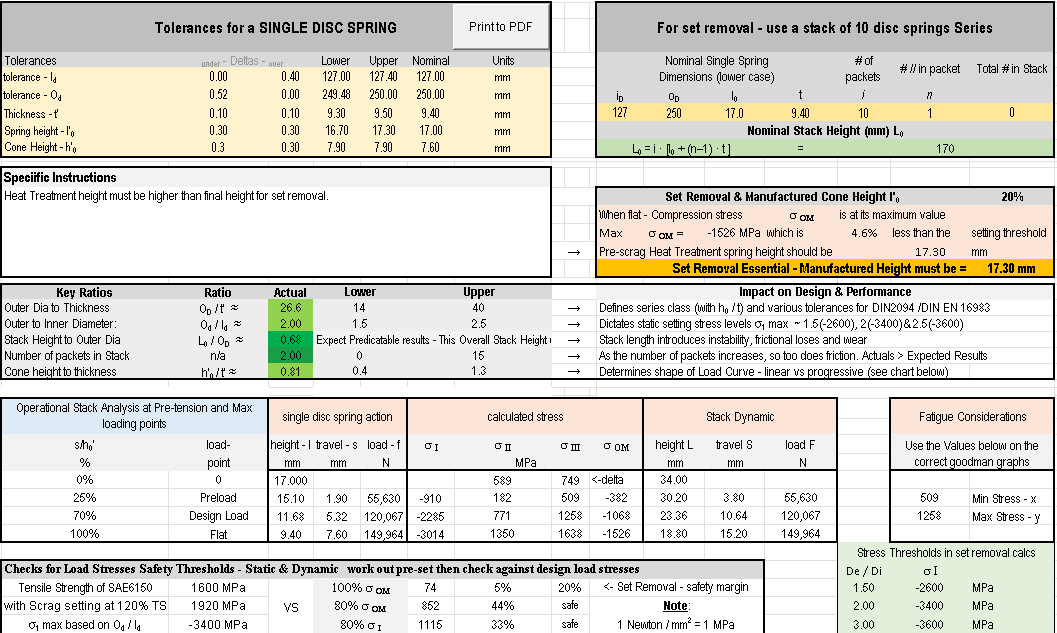
We use hydraulic presses to slowly form the machined disc spring to its heat treatment height, which is greater than the final design height. This allows us to carry out the set removal (presetting) step, which is generally so poorly understood, and is a reason why so many disc springs do not perform as expected.
Heat Treatment
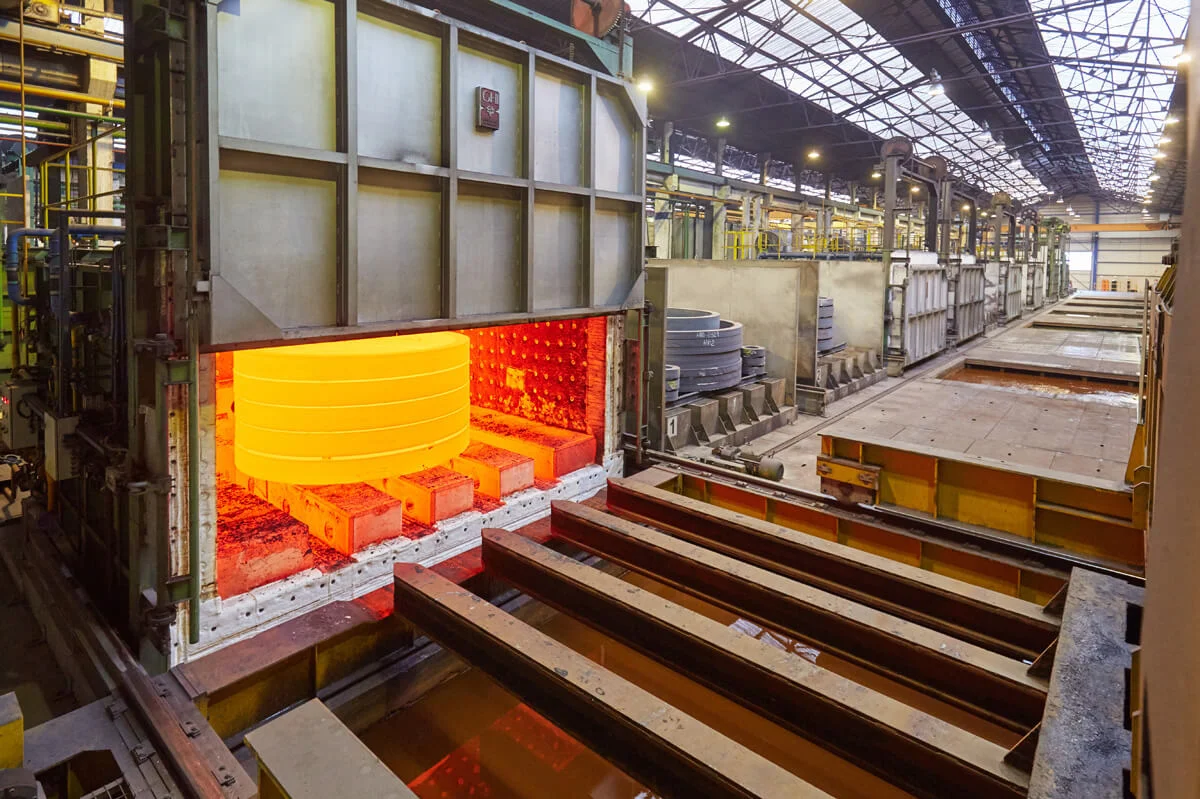
Whether it is INCONEL needing precipitation hardening or SAE 6150 needing quenching, it is the tempering that really makes the difference.
For economy of scale we outsource our heat treatment to the best outfit in the Southern Hemisphere: Macsteel.
Set Removal (Presetting)
At full compression, the calculated stress at the top inner edge of a disc spring is often higher than the yield strength of the hardened material. If nothing is done, the spring takes a permanent set in service and loses height and force. So after heat treatment every disc spring is pressed flat (preset). This deliberate, controlled plastic deformation takes out the set and leaves favourable residual stresses in the disc spring.
If this step is not done properly, disc springs relax and lose their height very quickly. This is also why, for bespoke disc springs, you will not find off-the-shelf stock with Reliable, and why we’d advise you to be somewhat circumspect about manufacturers who claim to have such stock ready for you.
Surface Treatment
We have two processes here:
- Shot peening: this puts the surface into compression, which slows the start and growth of fatigue cracks. DIN EN 16983 fatigue diagrams assume shot-peened disc springs.
- Corrosion protection: we apply a black oxide finish, which in our experience is superior to zinc phosphating for this purpose.

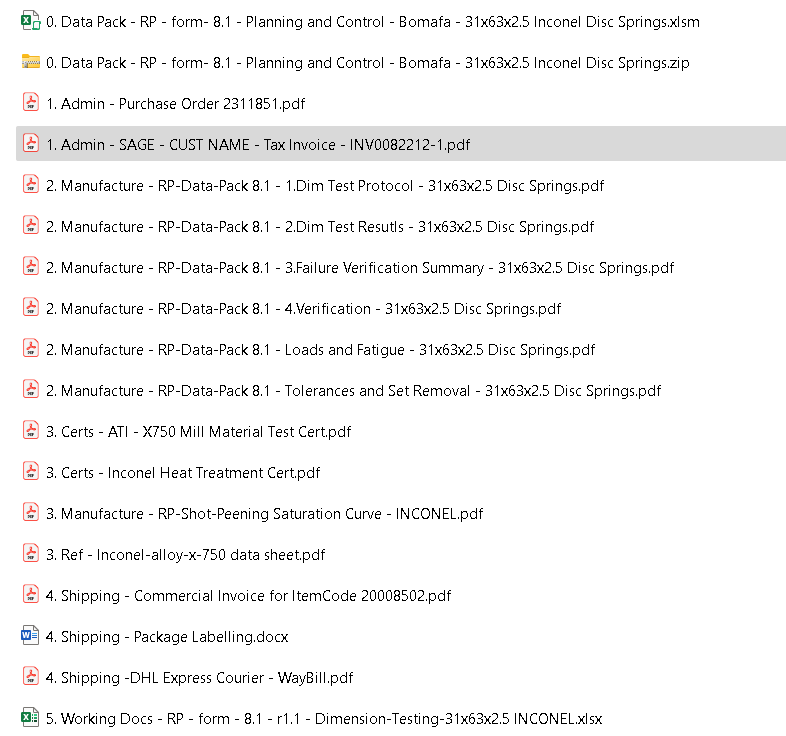
Quality Assurance Data Pack
Each project is only closed once the customer has reviewed the data pack and found that it meets their quality standards.
Packaging
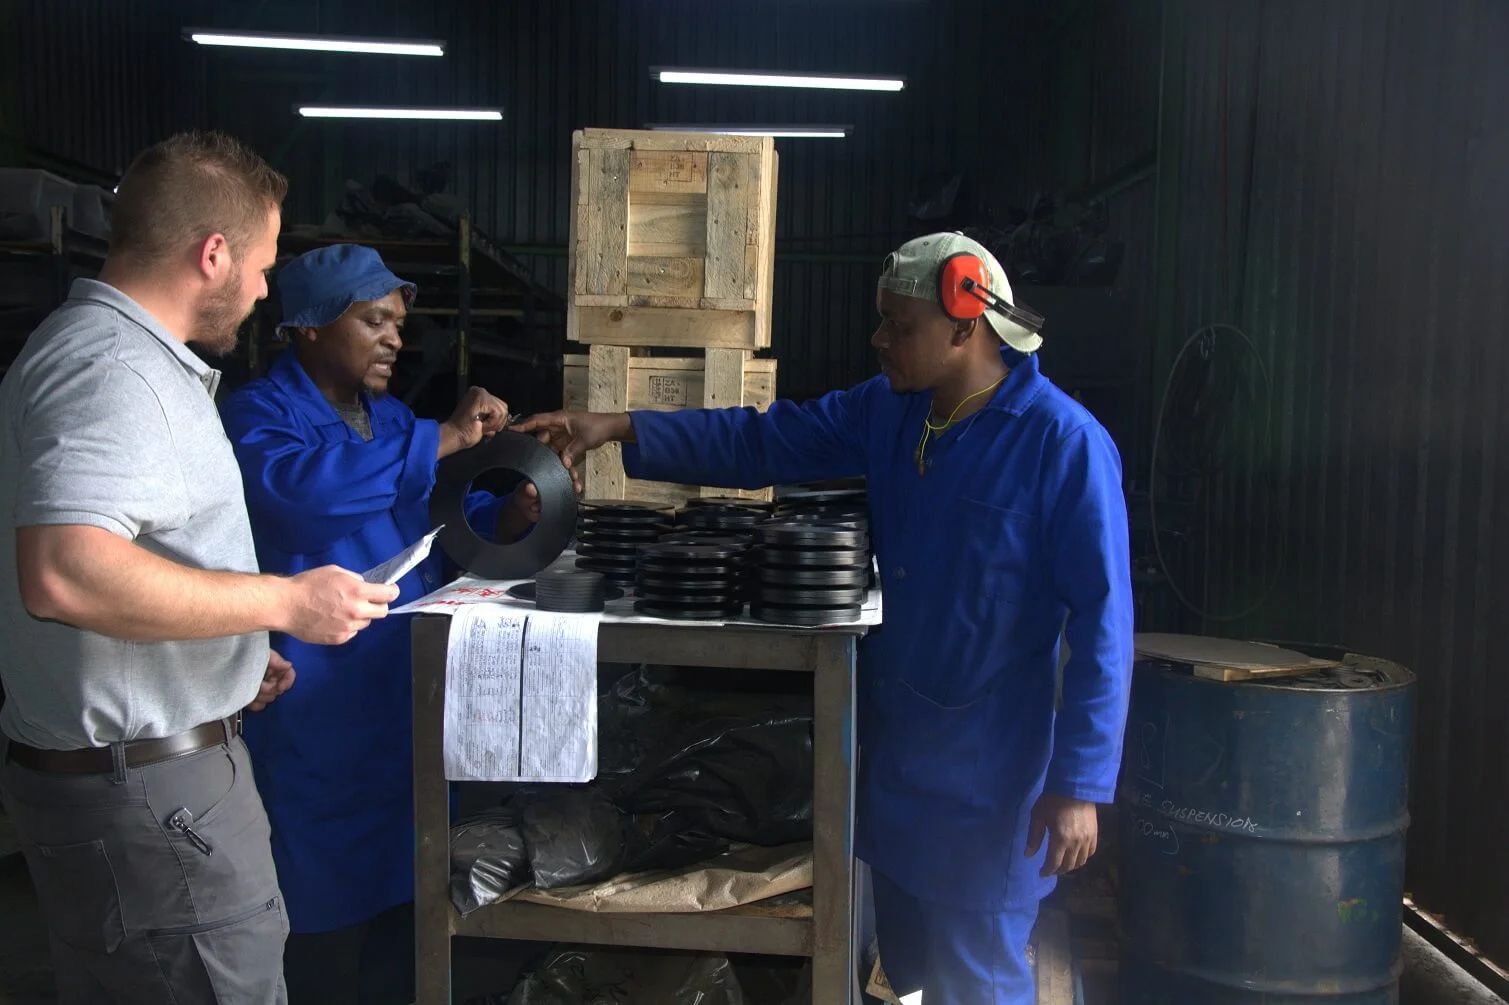
Our disc springs are packed into crates that never exceed 40 kg, and we try to fill each crate with the number of disc springs used in one stack. This helps clients when they install on site. (For smaller disc springs this is obviously not the case.) Each crate contains disc springs that have been:
- lightly oiled,
- packed in plastic bags in neat stacks,
- bubble wrapped,
- vacuum sealed, and
- packed into appropriately sized crates.
We are very aware of what can happen at customs if the wrong crating is used:
- our crating is ISPM 15 compliant and heat treated;
- every piece of wood is stamped;
- the crates are suitable for forklift handling;
- the crates are not waterproof, but their contents always are.
Shipping
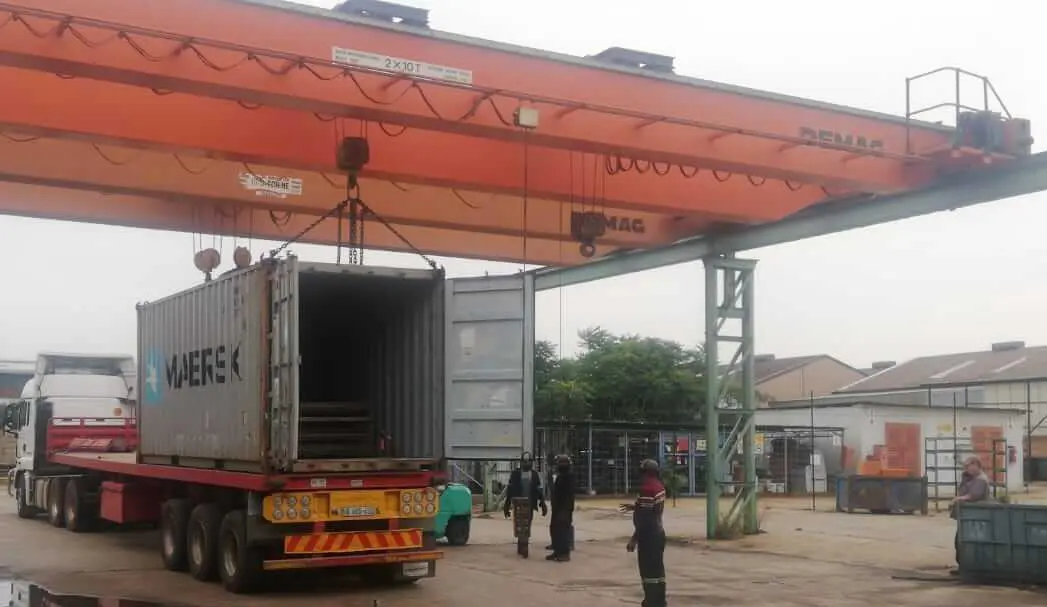
We can ship containers easily, because our infrastructure makes loading really easy.
Planning a project with bespoke disc springs?
Talk to us early. We’ll plan the design verification, hold points and delivery with you.